Quality Assurance
At Ripharma Laboratories Ltd., Quality Is Integral To Every Aspect Of Our Pharmaceutical Operations.
We are committed to the manufacturing, marketing and distribution of finished pharmaceutical formulations manufactured in compliance with established Good Manufacturing Practices (GMP), applicable pharmacopeial standards and relevant national and international regulatory requirements.
Our quality assurance framework is supported by strategic partnerships with licensed pharmaceutical manufacturing facilities, including facilities that have undergone inspections and audits by regulatory authorities in international markets and have secured the requisite regulatory approvals and manufacturing accreditations.
We place considerable emphasis on adherence to:
- Approved manufacturing practices
- Validated production processes
- Product quality specifications
- Stringent quality control procedures
Together, these ensure the safety, efficacy, consistency and reliability of our pharmaceutical portfolio.
Quality & Manufacturing Standards
-
International GMP Standards & Regulatory Approvals
Our manufacturing network includes facilities operating under internationally recognised GMP frameworks, including:
- WHO-GMP
- PIC/S GMP
- EU GMP
These regulatory frameworks establish requirements for pharmaceutical manufacturing, quality management systems, production operations and facility standards, providing a structured basis for maintaining compliance with applicable GMP requirements.
-
Quality Control & Product Conformity
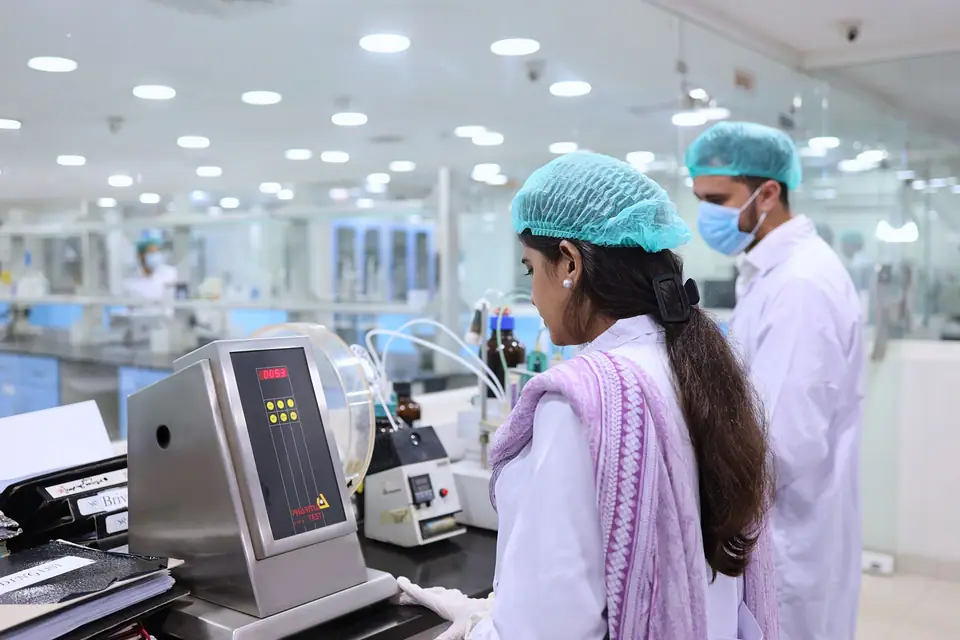
Finished pharmaceutical formulations are subjected to established quality control procedures and defined testing protocols to verify conformity with approved product specifications. Depending on the formulation and dosage form, testing encompasses:
- Physical parameters
- Chemical parameters
- Microbiological parameters
- Other applicable quality attributes
Batch-specific quality documentation, including Certificates of Analysis (COA), provides documented evidence of compliance with prescribed specifications and established quality requirements. These controls support product consistency and conformity across manufacturing batches.
-
Packaging, Labelling & Product Integrity
Packaging and labelling are governed by approved specifications and established quality checks to ensure:
- Suitability of packaging materials
- Accuracy of product identification
- Labelling compliance
- Integrity of the finished pack
Particular consideration is given to applicable market-specific packaging and labelling requirements, as well as the compatibility of packaging components with the product and its intended storage conditions. These measures help safeguard product quality and maintain the integrity of finished pharmaceutical formulations.
-
Storage, Handling & Distribution
The preservation of pharmaceutical quality extends beyond manufacturing and is dependent on appropriate storage, handling and distribution practices. Conditions are maintained in accordance with:
- The specified storage requirements of individual formulations
- Their stability characteristics
Where required, appropriate temperature-controlled storage and transportation arrangements are implemented to maintain product stability throughout the distribution chain.
Our Quality Commitment
We remain committed to upholding internationally recognised pharmaceutical quality standards and maintaining the reliability and consistency of our finished pharmaceutical portfolio across the markets we serve.